Authorship, review and evidence boundary
- Technical review
- East Baoyu Engineering Editorial Team
- Reviewed
- 2026-09-06
- Scope
- General engineering and procurement guidance. This article is not a project-specific design, capacity statement, certificate, warranty, code interpretation or contract requirement.
Evidence basis: Official and public references identified in the article. Project values and release decisions require qualified review under the applicable project responsibilities.
Read the Editorial PolicyGalvanizing repair inspection should start before anyone reaches for a silver coating. When hot-dip galvanized steel is cut, welded, mishandled or found with an uncoated area, preserve the as-found condition, confirm the governing product and contract route, bound every affected zone, and authorize the repair method. Only then should repair, reinspection and release begin. The decision is not whether the patch looks gray. It is whether local repair is permitted for that cause, extent and location, whether the procedure was followed, and whether evidence reconnects the repair to the item and downstream release. This guide provides that control route without setting a universal repair area, coating thickness, preparation grade or material.
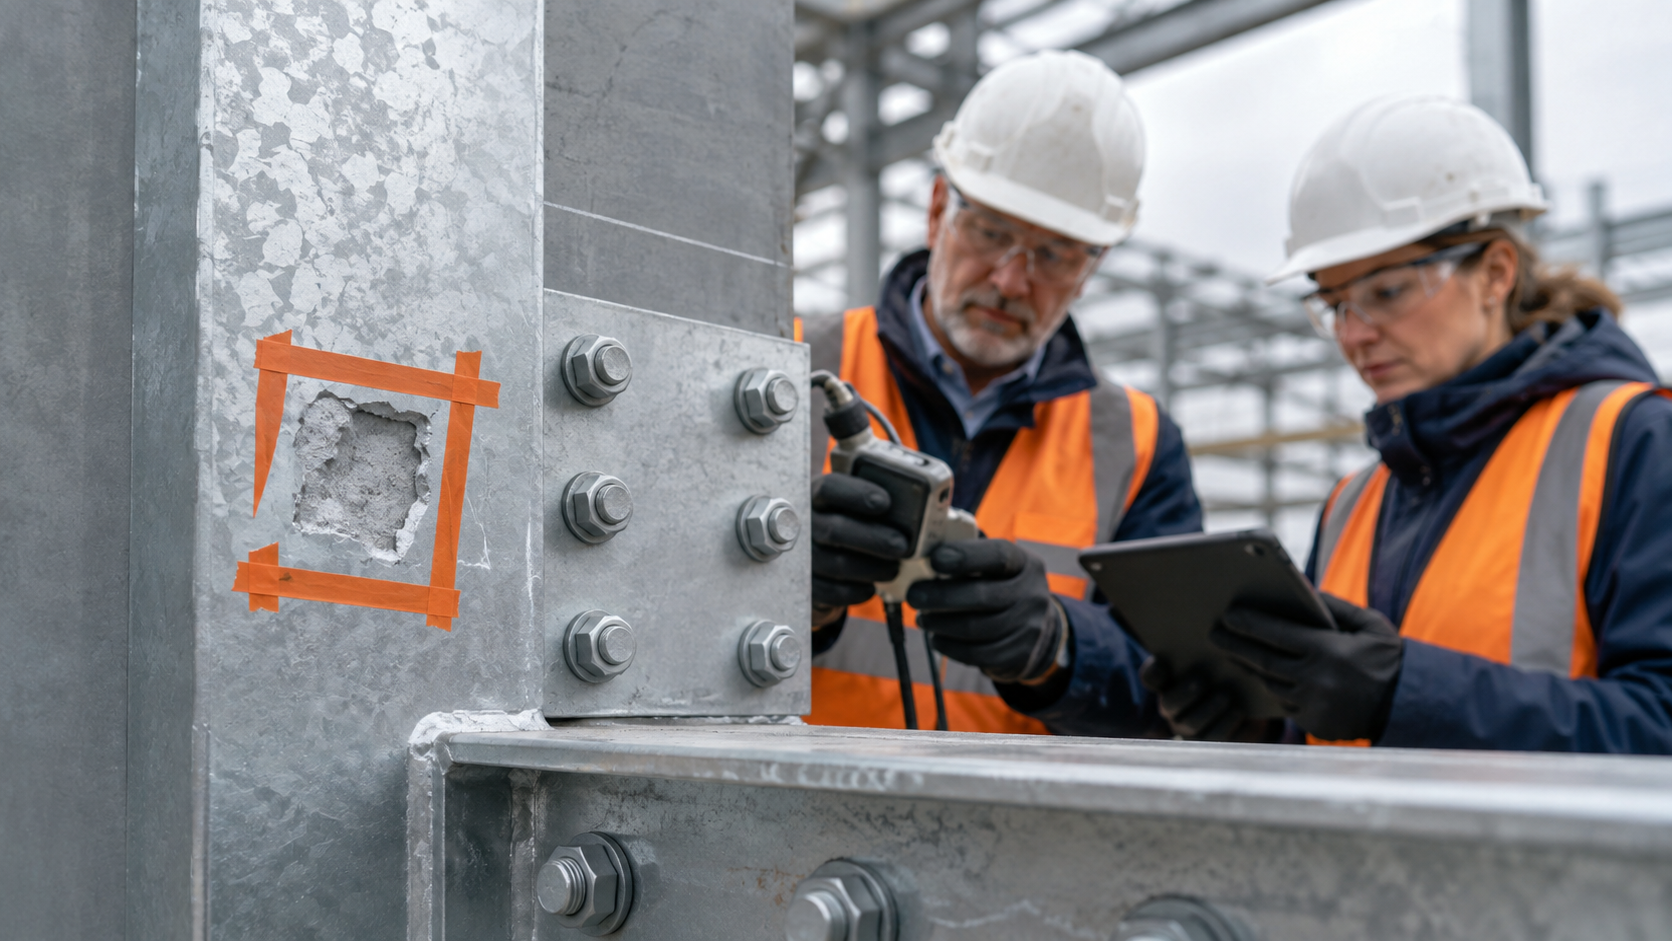
Featured image: AI-generated conceptual illustration of a bounded coating-damage inspection. It is not a real project, defect, test or acceptance record.
Preserve the As-Found State Before Surface Preparation
The first irreversible mistake is cleaning the area before recording what happened. Grinding, wire brushing, solvent cleaning or coating removal can erase the boundary between original galvanizing, exposed substrate, contamination, heat damage and an earlier repair. It can also destroy clues that connect one defect to a repeated handling or fabrication event.
Give the physical item a hold identity before surface preparation. Record the project or order reference, piece mark, serial or pack identity where available, exact member face and orientation, drawing detail, discovery time and current location. Photograph the area at context and close range with a controlled scale. Mark the perimeter in a way that does not conceal the surface. If the item is already erected, connect the record to its grid, elevation or assembly position.
Do not label every silver-surface problem as the same defect. An initial uncoated area points back to the galvanizing lot and original inspection. Abrasion or impact requires the handling event and nearby items to be checked. Field cutting, drilling or welding first needs the approved modification and any structural or welding disposition. An unknown touch-up needs its material and history identified before another layer is added. In every case, ask whether the issue is coating-only and which other items share the same cause.
A coating repair cannot close a bent plate, unauthorized hole, unacceptable weld or damaged connection. Separate the structural or fabrication disposition from the corrosion-protection disposition, even when both appear on the same member. The repaired coating should never become visual camouflage for an unresolved base-steel condition.
Decide Whether Local Repair Is an Authorized Route
Start with the actual product and contract, not a generic galvanizing note. ISO 1461:2022 specifies general properties and test methods for hot-dip galvanized coatings on fabricated iron and steel articles. Its public scope excludes continuously galvanized sheet, wire and mesh, tube or pipe galvanized in automatic plants, and products such as fasteners when specific standards apply. Its public contents include acceptance, renovation and damaged-area provisions, but the project still has to identify the adopted edition and any supplementary requirements.
For an ASTM order, ASTM A123/A123M-24 covers defined iron and steel products galvanized by the hot-dip process, including many fabricated products. Other products can follow different specifications. Confirm the product family before borrowing any repair criterion from an old report or unrelated component.
ASTM A780/A780M-20 is an active practice for repairing damaged and uncoated hot-dip galvanized areas on specified hardware, structural shapes and other products. Its public scope explicitly includes damage from welding, flame cutting, rough shipping and erection handling. It also states that the contracting parties should agree both the repair extent and the method. That makes local repair a controlled disposition, not an automatic right.
Use a release gate before work begins:
The project specification, purchase order, approved drawings, inspection and test plan, site procedure and applicable law determine who can approve each gate. The galvanizer, fabricator, erector, coating specialist, inspector, engineer, EPC and owner may hold different responsibilities. A repair record must show the actual authority rather than assume that the person applying the material can release the item.
Bound the Repair Zone and the Affected Population
The visible bare spot is not automatically the complete repair boundary. An impact can lift or crack adjacent coating. Thermal work can affect a wider zone than the cut or weld line. Preparation may enlarge the exposed substrate. A repeated jig, transport contact, lifting accessory or field detail can create the same condition on other items.
Build the boundary in two directions. First, work outward on the item until the inspection method has distinguished sound retained coating, suspect adjacent coating and exposed or prepared steel. Second, work outward through the process history until the team can explain which other items share the cause. Do not use a photograph alone to establish either boundary.
The repair population may be one marked area on one member, several locations on that member, every article in a handling batch, every connection with the same field modification, or an unresolved group awaiting screening. The project procedure should define how the population is inspected, expanded or reduced. Avoid inventing a universal distance, sample percentage or number of readings.
Before materials are issued, create a Repair Boundary Ledger. It should hold the item and physical location, as-found map, cause/event, shared-cause population, governing repair authorization, current hold status and linked records. Give every zone a unique identifier that remains visible through preparation and reinspection. If masking, access or assembly hides part of the boundary, resolve that constraint before execution. A complete record of an incomplete surface is not enough.
Select the Method from the Contract, Environment and Access
ASTM A780/A780M describes three repair-material families: zinc-based solders, paints containing zinc dust, and sprayed zinc. This list does not mean the three routes are interchangeable or suitable for every project. The method must match the governing product specification, permitted repair extent, service environment, geometry, access, later coating system, approved procedure and safety controls.
If the project follows an ISO route, use the contract-adopted renovation provisions and agreed procedure. Do not import ASTM language silently. If the project follows ASTM, do not reduce A780 to the product name printed on a can. The current material, surface preparation, application conditions and inspection requirements still need approval.
| Repair family named by ASTM A780/A780M | Questions before authorization | Execution evidence to retain | Reinspection focus to define |
|---|---|---|---|
| Zinc-based solder | Is this family permitted for the product, location and extent? Is the heating/application route compatible with the member and adjacent coating? | Approved procedure, exact material identity, preparation, operator, application record and required safety controls | Coverage, required thickness or other criterion, edge transition, adjacent coating and functional condition |
| Paint containing zinc dust | Is the exact product accepted for the exposure and any later coating? What preparation, mixing, application, environmental and cure controls apply? | Product/batch identity, approved data sheet, preparation evidence, ambient/surface records where required, application and cure record | Required dry-film or other acceptance data, continuity, cure, edge condition and compatibility with later work |
| Sprayed zinc or metallizing | Is the process, equipment, operator and access route approved for this item and location? How will surrounding work be protected? | Approved procedure, equipment/consumable identity, surface-preparation record, operator qualification where required and application log | Specified thickness/coverage evidence, boundary condition, adjacent coating and any required sealing or follow-on treatment |
Do not choose a method because it is fastest on site or gives the closest color match. Color is not proof of zinc content, preparation, applied thickness, cure, bond, continuity or service compatibility. Equally, do not claim that one family is universally superior. The accepted route is the one supported by the governing documents and the conditions of the actual repair.
ASTM A780/A780M states that it does not address every safety concern. Before surface preparation or application, apply the approved site safety system, applicable regulations, product instructions and safety data sheets. Heat, fumes, spray, dust, solvents, access and nearby operations must be assessed by the accountable parties for the chosen method. This article is not a work method or safety procedure.
Issue a Repair Control Card Before Execution
A repair procedure describes how approved work should be performed. A Repair Control Card proves how one identified zone moved through that procedure. Issue the card while the as-found condition is still visible, and prevent the repair from starting until its mandatory fields are complete.
| Control-card block | Minimum project-specific information | Hold trigger |
|---|---|---|
| Identity | Project/order, item, repair-zone ID, drawing/detail, physical location and current status | Item or zone cannot be located unambiguously |
| Condition and cause | As-found map, photographs, cause/event, base-steel or weld disposition and affected population | Structural, welding, dimensional or cause assessment remains open |
| Authority | Governing specification/edition, repair clause, disposition, approving roles and intervention point | Local repair or the selected method lacks authorization |
| Procedure and material | Current procedure revision, repair family, product/consumable and batch, preparation and application requirements | Material, batch, procedure or compatibility is unverified |
| Execution conditions | Operator, date/time, surface state, access and environment/process values required by the approved method | A required condition is missing or outside the procedure |
| Inspection plan | Inspection stages, instrument/method, locations, decision rule, witness/hold status and acceptance authority | Acceptance basis or required attendance is undefined |
| Closure | Actual results, photographs where required, repair and reinspection signatures, linked NCR and final release destination | Any required result, record or authority remains open |
Keep the card concise enough to use at the workface. Long specifications can remain controlled references. The card should point to them by title and revision, capture the item-specific values and make the next hold point unmistakable.
Do not prefill acceptance with “OK,” copy instrument data from another repair, or let a generic daily report replace zone identity. If preparation reveals a larger defect, cracked coating, deeper base-metal damage or an unrecognized prior repair, stop and revise the boundary and disposition before continuing.
Reinspect the Repair and the Adjacent Coating
Reinspection asks more than “Was material applied?” It verifies identity, authorization, execution and the final physical state. Start by confirming that the repaired zone is the one authorized, that its final boundary remains within the permitted route, and that any structural, weld or dimensional condition has a separate closed disposition.
Where a magnetic thickness method is adopted, ISO 2178:2016 specifies nondestructive measurement of non-magnetizable coatings on magnetizable base metals. ISO currently lists the edition as published and under systematic review. The method’s applicability, instrument, verification, adjustment, measurement locations, grouping and acceptance calculation still come from the governing repair and inspection documents. One convenient reading does not represent an entire patch.
Use the reinspection matrix to prevent evidence gaps:
| Release question | Evidence expected | Failure state |
|---|---|---|
| Was the correct zone repaired? | Item and zone identity matched to the as-found map and authorization | Result cannot be traced to the physical repair |
| Did preparation expose a different condition? | Preparation-stage observation and any revised boundary or disposition | Original approval no longer represents the final repair extent |
| Was the approved material and procedure used? | Procedure revision, product/consumable batch, operator and execution record | Similar-looking material or an uncontrolled method was substituted |
| Were required application conditions met? | Method-specific surface, environment, application and cure/cooling records | Missing or out-of-range conditions remain unresolved |
| Does the repair satisfy the controlled criteria? | Required visual, dimensional, thickness, continuity or other test results with raw data and locations | Only “checked” or an isolated result is recorded |
| Is surrounding coating still sound? | Examination of the repair edge and adjacent original coating over the approved extent | Preparation or application damage lies outside the recorded zone |
| Does the item still fit and function? | Required hole, thread, faying-surface, connection, clearance or dimensional check | Coating closure hides an interface problem |
| Can the item be released downstream? | Closed exceptions, authorized signature, date, status and destination link | Repair passes locally but the item or population remains contractually held |
Preserve the original failed or damaged state alongside the final result. Do not overwrite photographs, delete low readings or replace the first record with a clean revision. If the repair fails, retain the as-found and repair evidence, extend containment as required, and issue a new authorized disposition. The audit trail should show why the status changed.
Release the Item Without Erasing the Damage History
Release only the item and repair population supported by the evidence. Use explicit outcomes such as accepted after recorded repair, held for missing evidence, returned for reprocess or re-galvanizing, rejected/replaced, or accepted under an authorized concession. The contract defines the permitted terms and decision authority.
Connect the repair-zone ID to the item release note, packing list, erection record or handover dossier. Where a field modification created the damage, retain the approved drawing revision, welding or machining record and coating repair as linked but distinct closures. Where repeated handling caused the issue, close the affected population and corrective action rather than releasing only the first repaired member.
The final decision boundary is simple: a local repair is complete only when the project can reconstruct the original condition, explain why repair was allowed, identify what material and procedure were used, reproduce the inspection decision, and show who released the exact item. A gray patch without that chain is unfinished evidence.
Related Resources
- Quality & Manufacturing — East Baoyu's current quality context and inquiry route.
- Galvanizing Inspection: A Release Checklist for Steel Buyers — the broad product, lot, thickness, appearance and release inspection route.
- Structural Steel Galvanizing: Design Before the Bath — fabrication-readiness, venting, drainage, distortion and interface decisions before galvanizing.
- Coating Inspection Report: Trace the Release Evidence — record architecture for protective-coating application and release.
- Steel Fabrication ITP — integrating material, welding, coating and final release evidence.
References
- International Organization for Standardization, ISO 1461:2022 — Hot dip galvanized coatings on fabricated iron and steel articles.
- ASTM International, ASTM A123/A123M-24 — Zinc coatings on iron and steel products.
- ASTM International, ASTM A780/A780M-20 — Repair of damaged and uncoated hot-dip galvanized areas.
- International Organization for Standardization, ISO 2178:2016 — Magnetic measurement of coating thickness.
Next Step
For a supplier-side review, send the project country, governing specification and edition, item list and drawings, repair-zone photographs and map, as-found cause, affected population, structural or welding disposition, proposed repair procedure and material, inspection and test plan, required records, release roles and the decision you need. East Baoyu can identify missing fabrication, coating, identity and document interfaces within the agreed supply scope. The project engineer, coating specialist, site safety team, inspector, EPC and owner retain responsibility for repair approval, execution controls, inspection criteria and final acceptance.
Email: info@baolaipipes.com
References, disclosure and change record
References and further verification
- https://www.iso.org/standard/81435.html
- https://store.astm.org/a0123_a0123m-24.html
- https://store.astm.org/a0780_a0780m-20.html
- https://www.iso.org/standard/63004.html
- https://eastbaoyu.com/quality/
- https://eastbaoyu.com/galvanizing-inspection-steel-release/
- https://eastbaoyu.com/structural-steel-galvanizing/
- https://eastbaoyu.com/coating-inspection-report/
- https://eastbaoyu.com/steel-fabrication-itp-mtc-wps-ndt-coating/
Disclosure: East Baoyu manufactures and supplies products discussed on this website. Structured drafting tools may assist research and editing, but technical claims, project inputs and release decisions require qualified review under the applicable project responsibilities.
Version 1.0: Scheduled as EB50-045 on 2026-09-06.
View the public Content Change Log · Corrections: info@baolaipipes.com